
Process
Start-up and shutdown — the hours when plants break
Why most process incidents happen during transitions rather than steady running, what purging and inerting are protecting against, why a controlled shutdown and a trip are not the same event, and why the first start-up after a turnaround is the most dangerous shift of the year.
A plant spends almost all of its life running steadily, and a small fraction of it starting up or shutting down. A disproportionate share of serious incidents happens in that small fraction.
Why transitions are the dangerous part
Steady operation is the condition everything was designed for. Every control loop is tuned for it, every protection is set around it, every operator knows what the screens should look like.
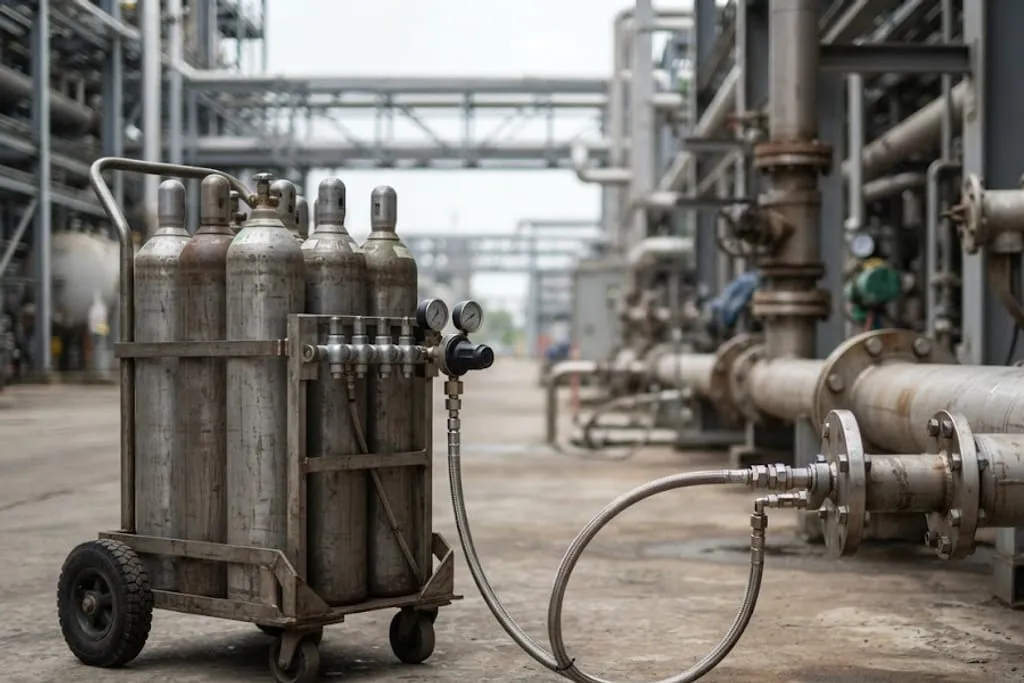
Purging and inerting
Before hydrocarbon enters equipment that has been open, the air has to come out.
The reason is the flammable range. A vessel full of air, filled with hydrocarbon, passes through the range between too lean to burn and too rich to burn — and it spends that passage as an ignitable mixture inside a closed vessel.
Warming, cooling and the rate of change
Equipment tolerates temperature; it does not always tolerate changing temperature quickly.
Differential expansion between a thick flange and a thin pipe, between tube and shell in an exchanger, or between refractory and steel in a fired heater produces stresses that steady operation never imposes. Procedures therefore specify heating and cooling rates, not just target temperatures.
Fired heaters have their own constraints — refractory dry-out on a new heater takes days, and a cold-start ramp is specified in degrees per hour. See fired heaters.
Controlled shutdown versus a trip
They are not the same event and should not be treated as interchangeable.
A trip is the safety system doing its job: removing energy and feed as quickly as possible because something has gone outside a safe limit. It is fast and it is blunt.
A controlled shutdown reaches the same end state in an order that equipment can tolerate — reducing rates, letting machines run down through their sequences, cooling at a controlled ramp, depressuring deliberately.
The first start-up after a turnaround
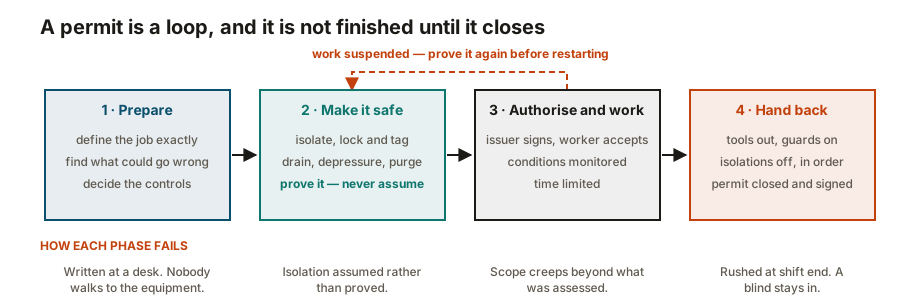
Of all the transitions a plant makes, this is the one that concentrates the risk.
Cleaning out what construction left behind
New or rebuilt pipework contains what was left in it during fabrication: welding rod stubs, grinding dust, mill scale, rags, and occasionally gloves and hand tools.
Air blowing, steam blowing, water flushing or chemical cleaning removes it before the system is commissioned, with temporary strainers left in the suction of every machine for the first period of running.
Where this connects
Transitions are where alarm floods happen, where overrides are applied, and where relief systems see their most unusual cases. They are also where the greatest share of what incident investigation examines takes place.
What to take away
- Transitions carry the risk, because conditions are abnormal, controls are manual, protections may be bypassed and people are under pressure.
- Purge before admitting hydrocarbon, and before admitting air. The flammable range is crossed in both directions.
- Rate of change matters, not just the target. Differential expansion is a transition-only stress.
- Warm steam lines slowly with drains open. Water hammer splits pipework.
- A trip protects people; a controlled shutdown protects the plant too. Use the planned route where there is a choice.
- The first start-up after a turnaround is the highest-risk shift — every reinstatement error surfaces at once.
- Clean out construction debris, and actually inspect the temporary strainers before removing them.
Check your understanding
7 questions. Nothing is recorded — this is just for you.