
Mechanical
Preheat and post-weld heat treatment — hydrogen, hardness, and reading the chart
What preheat is actually for, why interpass temperature has a ceiling as well as a floor, when PWHT is required and when it may be exempted, how to read a chart recorder trace against the specified cycle, and the hardness survey that decides it in sour service.
Standards referencedASME B31.3ASME Section IXNACE MR0175API 577
Two thermal cycles bracket a weld: one before it and one after. They are specified separately, for different reasons, and both are routinely treated as formalities by people who have not had to explain a cracked joint.
Preheat
What it is for
Not to make the metal easier to melt. To slow the cooling rate.
A thick cold section acts as a heat sink and pulls the heat out of a weld very quickly. Fast cooling does two bad things at once:
- Hydrogen is trapped. Hydrogen dissolves into the molten pool from moisture, oil, rust or damp electrodes. Given time it diffuses out. Cooled fast, it stays — and hydrogen in a hard structure under residual stress is the recipe for delayed cracking, which can appear days after the weld looked perfect.
- A hard, brittle structure forms in the heat-affected zone.
Preheat attacks both by slowing the cooling. Which is why it is specified by material and thickness — the two things that set the cooling rate — and not by how cold the morning feels.
Interpass temperature
Preheat has a minimum, maintained throughout. Interpass also has a maximum.
Measuring it
Post-weld heat treatment
When it is required
Driven principally by thickness, with material group setting where the threshold falls. B31.3 states requirements and exemptions below stated thicknesses; carbon steel is exempt well above where the chrome-moly alloys have long since required it.
Service can add its own requirement on top — sour service being the obvious case.
What it does
Holding the joint at temperature lets residual stresses relax, tempers the hard structure left by rapid cooling, and drives off remaining hydrogen.
Reading the chart
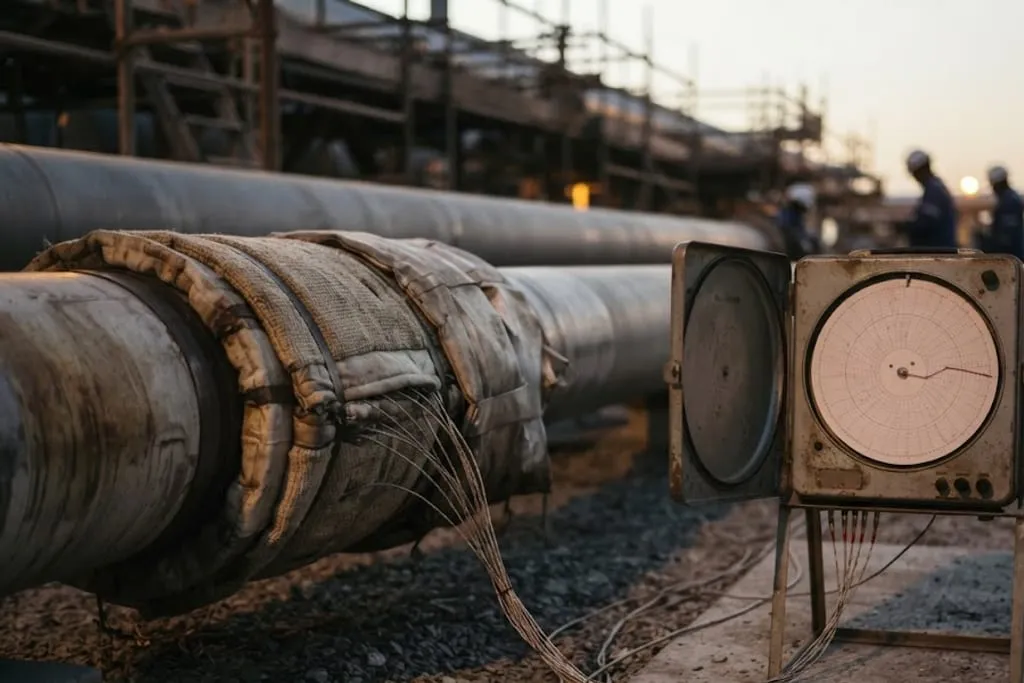
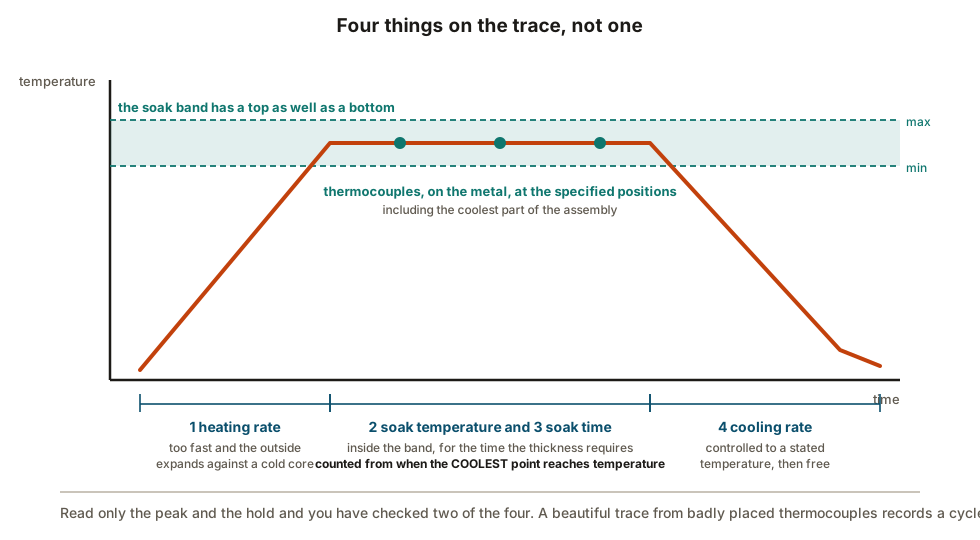
The record is a trace, and there are four things on it, not one.
| What to read | Why |
|---|---|
| Heating rate | Too fast and the outside expands against a cold core, creating its own stresses. The spec controls it |
| Soak temperature | Within the specified band — and the band has a top as well as a bottom |
| Soak time | By thickness, and it starts when the coolest monitored point reaches temperature |
| Cooling rate | Controlled down to a stated temperature, then free |
Reading only the peak and the hold time misses half of what the cycle was meant to control.
Thermocouples
The trace is evidence about the metal only if the sensors were on the metal, at the positions the procedure specified — including the coolest part of the assembly, which is what the soak time is counted from.
A beautiful chart from badly placed thermocouples records a cycle that part of the joint never experienced. Placement is part of the record, not a detail of the setup.
Hardness, and sour service
Where the service limits hardness — sour service above all, under NACE MR0175 and ISO 15156 — a hardness survey is the verification that the thermal cycles did their job.
Hardness is the practical proxy for susceptibility to sulphide stress cracking, and the heat-affected zone is where an uncontrolled cycle leaves a hard band. On those lines, preheat and PWHT stop being paperwork and become integrity items with a measurement attached.
See material degradation.
Welding to a spool that has already been treated
The auditable record
For PWHT: the chart trace, the thermocouple positions, the equipment and operator, the procedure, and — the one most often missing — the joints it covered, by weld number.
A chart that cannot be tied to specific welds proves a cycle happened somewhere. That is not the same as proving it happened to this joint, and at handover it is the difference between a closed line and an open question.
What to take away
- Preheat slows cooling — against hydrogen cracking and a hard HAZ. Not to help melting.
- Interpass has a maximum too, protecting toughness.
- Measure preheat through the section, not beside the torch.
- PWHT is driven by thickness and material group, with service on top.
- It relaxes stress and tempers hardness — and repairs nothing.
- Read the chart for ramp, soak band, soak time and cooling, not just the peak.
- Thermocouple placement is part of the evidence; soak counts from the coolest point.
- Hardness survey is the verification in sour service.
- Welding to a treated spool undoes it locally — clamp instead.
- Tie every chart to weld numbers.
Check your understanding
10 questions. Nothing is recorded — this is just for you.